
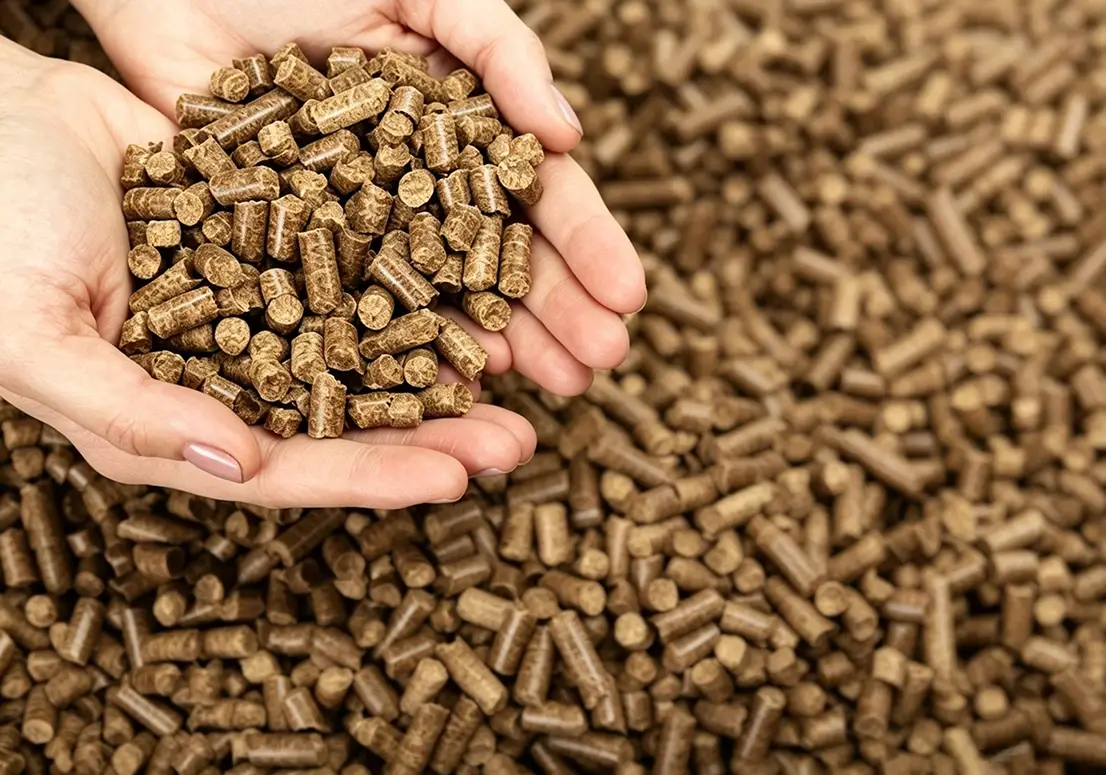
Empty fruit bunches, commonly known as EFB, are an important biomass residue generated by palm oil mills. As palm oil production continues to generate large quantities of this material, converting EFB into fuel pellets provides a practical way to improve biomass utilization and produce a standardized renewable fuel.
However, producing high-quality EFB pellets is not simply a matter of feeding EFB into a pellet mill. The quality of the final pellets depends on a combination of raw material characteristics, pretreatment, moisture control, particle size, pellet mill settings, die design, cooling, screening, and storage.
For producers planning an EFB pellet plant, understanding these factors is important for maintaining consistent pellet strength, density, dimensions, and storage stability. It can also help reduce fines, equipment wear, energy consumption, and production losses.
This article explains the major factors that affect EFB pellet quality and how each factor can be controlled during commercial production.
What Is EFB Pellet Quality?
EFB pellet quality describes the physical characteristics and performance of pellets made from empty fruit bunches.
For biomass fuel applications, important quality indicators include:
- Moisture content
- Pellet density
- Mechanical durability
- Pellet hardness
- Pellet diameter
- Pellet length
- Percentage of fines
- Surface appearance
- Storage stability
- Combustion characteristics
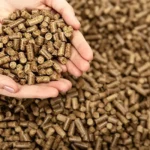
A good EFB pellet should have relatively consistent dimensions, sufficient mechanical strength, low levels of loose fines, and appropriate moisture for transportation and storage.
The exact specifications depend on the intended application. Pellets used in industrial boilers may have different requirements from those intended for smaller biomass heating systems.
1. EFB Raw Material Quality
The quality of the finished pellet starts with the quality of the EFB itself.
EFB characteristics can vary depending on the palm oil processing process, storage conditions, moisture level, palm variety, and collection method.
For example, EFB that has been exposed to rain may contain more moisture and contaminants than material collected and stored under controlled conditions.
Important raw material characteristics include:
- Moisture content
- Fiber structure
- Particle size
- Bulk density
- Ash-forming contaminants
- Organic composition
- Storage condition
Maintaining relatively consistent feedstock characteristics makes it easier to produce stable pellets.
2. Moisture Content
Moisture is one of the most important factors affecting EFB pellet quality.
During pelletizing, moisture influences how biomass particles move through the die and how well they bind together under pressure.
If EFB contains too much moisture, several problems may occur:
- Weak pellet formation
- Increased energy consumption
- Poor pellet durability
- Difficulty maintaining stable production
- Higher drying requirements
On the other hand, excessively dry material may also produce fragile pellets because the particles may not form a sufficiently stable structure during compression.
Therefore, the goal is to maintain a suitable and consistent moisture level before pelletizing.
Why Consistent Moisture Matters
Average moisture content alone is not enough.
If one portion of EFB is very wet while another portion is relatively dry, the pellet mill may receive inconsistent material. This can cause fluctuations in pellet density and mechanical strength.
A properly designed drying system should therefore provide uniform moisture reduction rather than simply removing as much water as possible.
3. Drying Performance
EFB often requires drying before pelletizing, especially when it comes directly from palm oil processing.
A rotary drum dryer can be used for continuous industrial drying.
The performance of the dryer depends on:
- Initial moisture
- Target moisture
- Material throughput
- Hot-air temperature
- Residence time
- Airflow
- Heat source
- Drum configuration
Poor drying can directly affect pellet quality.
If the material leaving the dryer has inconsistent moisture, the pellet mill will have difficulty maintaining stable operating conditions.
An efficient drying system should therefore be designed according to the actual moisture and capacity requirements of the EFB pellet plant.
4. Particle Size
Particle size has a significant influence on pellet quality.
EFB contains long fibers and irregular pieces that may be too large for efficient pellet formation.
Large particles can cause:
- Poor compression
- Uneven pellet density
- Increased die blockage
- Irregular pellet surfaces
- Higher fines content
A crushing or grinding system is therefore normally installed before the pellet mill.
The material should be reduced to an appropriate size without unnecessary over-grinding.
Excessive grinding can increase electricity consumption without providing a corresponding improvement in pellet quality.
The appropriate particle size depends on the pellet diameter, die design, raw material characteristics, and pellet mill configuration.
5. Fiber Length
Unlike some fine wood residues, EFB has a naturally fibrous structure.
Long fibers can make the material difficult to feed and compress.
They may also become entangled and create unstable material flow.
A suitable shredding process can break long fibers into shorter pieces before fine grinding.
The objective is to create a more uniform feedstock that can enter the pellet mill consistently.
However, the material does not necessarily need to be converted into extremely fine powder. The ideal preparation level should balance pellet quality with grinding energy consumption.
6. Raw Material Cleanliness
Foreign materials can have a significant effect on EFB pellet quality.
Depending on collection and storage conditions, EFB may contain:
- Sand
- Soil
- Stones
- Metal
- Plastic
- Other processing residues
These materials can increase ash content and reduce the quality of biomass fuel.
Hard contaminants can also damage grinders, pellet mill dies, and rollers.
A cleaning system should therefore be incorporated into the production line.
Magnetic separators can be used to remove ferrous metal particles, while screening and other separation equipment can help remove larger contaminants.
7. Natural Binding Characteristics
Biomass pellets are formed through the combination of pressure, friction, heat, moisture, and the natural binding properties of the feedstock.
EFB contains natural components that can contribute to pellet formation when the material is properly prepared.
The compression process rearranges and compacts the particles into a dense structure.
This means that pellet quality does not depend only on the pellet mill’s mechanical pressure. Raw material preparation also determines how effectively the natural binding properties of EFB can be utilized.
If moisture or particle size is unsuitable, the natural binding effect may not be fully realized.
8. Pellet Mill Design
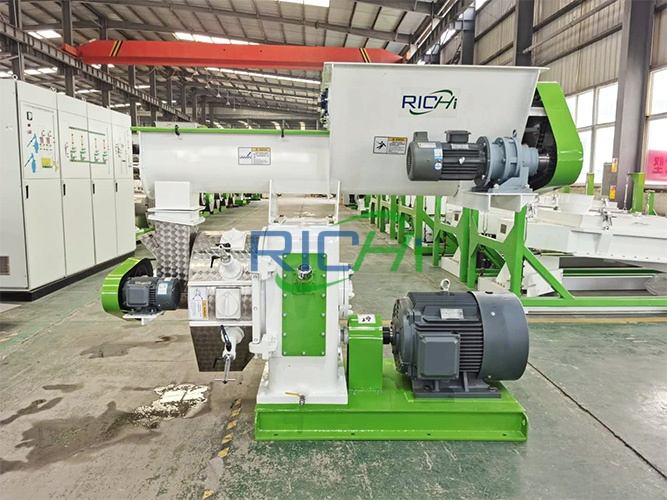
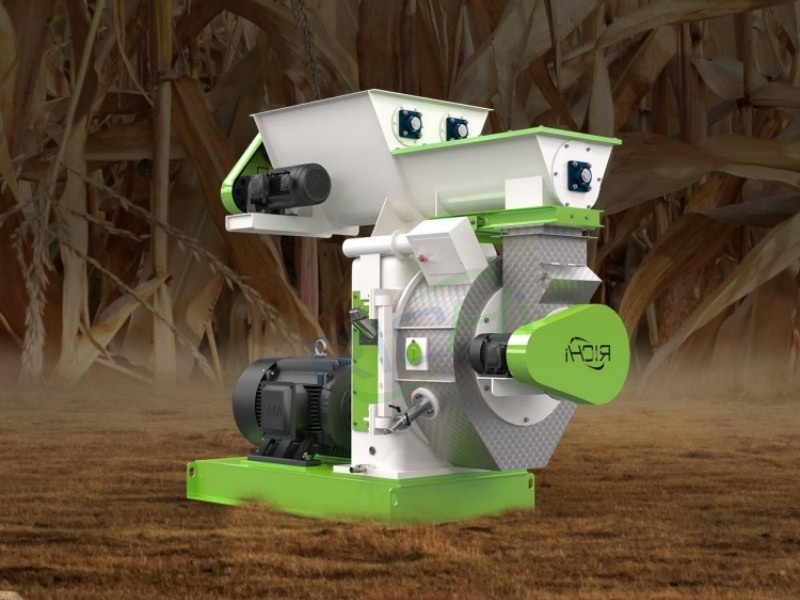
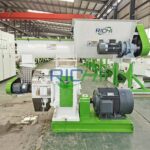
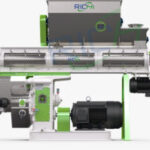
The EFB pelleting machine is the core piece of equipment in EFB pellet production.
Different pellet mills may have different die structures, roller systems, drive systems, and feeding arrangements.
When selecting equipment, producers should consider:
- Required capacity
- EFB characteristics
- Pellet diameter
- Moisture level
- Particle size
- Die compression ratio
- Motor power
- Roller design
- Operating hours
A pellet mill should be selected according to the actual material and production target rather than relying solely on theoretical capacity.
For large commercial EFB pellet plants, heavy-duty ring die pellet mills are commonly considered because they are designed for continuous industrial production.
(Learn more: https://richipelletizer.com/efb-pellet-machine)
9. Die Compression Ratio
The die compression ratio affects how strongly the EFB particles are compressed.
A suitable compression ratio can help produce dense and durable pellets.
If the compression ratio is too low, the pellets may be too loose and generate excessive fines.
If it is too high, several issues may appear:
- Higher power consumption
- Greater friction
- Increased die temperature
- Faster wear
- Reduced production stability
Therefore, the die should be selected according to EFB characteristics and the desired pellet specifications.
The correct compression ratio represents a balance between pellet durability, production capacity, energy consumption, and component life.
10. Die Hole Diameter
The diameter of the die holes determines the basic diameter of the finished pellets.
Different applications may require different pellet sizes.
For example, industrial fuel users may have different requirements from smaller heating applications.
Die hole diameter should therefore be selected based on:
- Final application
- Customer requirements
- Combustion equipment
- Pellet density
- Required production capacity
Using an unsuitable die can lead to inconsistent pellet formation and unnecessary energy consumption.
11. Roller Condition
The rollers work together with the die to compress EFB into pellets.
As the pellet mill operates, roller surfaces gradually wear.
Worn rollers may result in:
- Reduced compression
- Lower output
- More fines
- Uneven pellet density
- Higher electricity consumption
Regular inspection is therefore essential.
The roller surface should be maintained in good condition, and replacement should be considered when wear begins to affect production stability.
12. Die Condition
The die is another critical wear component.
Over time, die holes can become worn or damaged.
This can change the resistance experienced by the material and affect pellet formation.
Signs of die-related quality problems may include:
- Increased fines
- Lower pellet durability
- Irregular pellet dimensions
- Reduced capacity
- Higher motor load
Regular inspection can help identify these problems early.
Using high-quality wear-resistant die materials can also help maintain stable production over longer operating periods.
13. Roller-to-Die Clearance
The clearance between the roller and die must be properly adjusted.
Excessive clearance may reduce effective compression and result in weaker pellets.
Insufficient clearance can increase friction and accelerate wear.
Incorrect clearance can therefore affect both pellet quality and equipment service life.
The exact setting depends on the pellet mill design and should follow the manufacturer’s operating recommendations.
14. Feeding Rate
The feeding rate affects how much EFB enters the compression chamber at a given time.
If the feeding rate is too high, the pellet mill may become overloaded.
If it is too low, production capacity may fall and the compression process may become unstable.
An appropriate feeding rate should allow the pellet mill to operate within a stable load range.
Variable-frequency feeding systems can provide better control over material flow and help operators respond to changes in raw material characteristics.
15. Stable Material Flow
EFB is lightweight and fibrous, which can create feeding challenges.
The material may bridge inside the hopper or form uneven flows.
Unstable feeding can result in fluctuations in:
- Motor current
- Pellet density
- Pellet length
- Production capacity
- Fines percentage
An appropriate hopper design, agitator, screw feeder, and anti-bridging system can help maintain consistent material flow.
For larger production lines, automatic feeding control can further improve stability.
16. Pellet Mill Operating Temperature
Temperature generated during pelletizing can affect pellet formation.
As EFB passes through the die under pressure, friction generates heat.
The actual operating temperature depends on:
- Moisture
- Feed rate
- Compression ratio
- Die design
- Material properties
- Machine speed
Stable temperature conditions can contribute to consistent pellet formation.
Sudden changes may indicate problems with moisture, feeding, die condition, or machine loading.
17. Pellet Density
Density is an important physical characteristic of fuel pellets.
Higher-density pellets generally occupy less storage space for the same mass and may be easier to transport.
Pellet density is influenced by:
- Raw material moisture
- Particle size
- Compression ratio
- Die design
- Pellet mill pressure
- Material composition
However, maximizing density is not always the only objective.
The production system should balance density with durability, energy consumption, and equipment wear.
18. Pellet Durability
Pellet durability describes how well pellets resist breaking during handling, transportation, and storage.
Low durability can result in excessive fines.
Factors affecting durability include:
- Moisture
- Particle size
- Compression
- Die condition
- Roller condition
- Cooling
- Pellet structure
If pellets appear intact when they leave the pellet mill but generate significant fines during transportation, the cooling, screening, or compression conditions may need to be reviewed.
19. Cooling Process
Fresh pellets leave the pellet mill at elevated temperatures.
They should be cooled before screening and packaging.
A suitable pellet cooler can help stabilize the pellet structure and moisture.
Insufficient cooling may result in:
- Increased pellet breakage
- Moisture migration
- Condensation
- Storage problems
- Lower final quality
For commercial production, a counterflow cooler is commonly used because it can provide continuous and efficient cooling.
20. Screening Efficiency
After cooling, the pellets should pass through a screening process.
Screening removes:
- Fines
- Broken pellets
- Undersized material
- Other unwanted particles
Efficient screening improves the appearance and consistency of the finished product.
Fines can often be returned to the pelletizing process, allowing producers to improve material utilization rather than treating them as waste.
21. Pellet Length
Pellet length is another quality consideration.
Pellets that are excessively long may be difficult to handle or feed into some combustion systems.
Very short pellets may increase the percentage of fines.
Pellet length can be influenced by:
- Die design
- Cutter position
- Pellet mill operating conditions
- Material characteristics
The production line should therefore be adjusted according to the requirements of the final user.
22. Storage Conditions
Pellet quality can change after production.
EFB pellets should be protected from excessive moisture during transportation and storage.
Poor storage conditions may cause pellets to absorb moisture, lose mechanical strength, or break apart.
Suitable storage should therefore provide:
- Protection from rain
- Low exposure to humidity
- Good ventilation
- Clean surroundings
- Appropriate packaging
For long-distance transportation, packaging and loading methods should also minimize mechanical damage.
23. Production Line Balance
Even when the pellet mill itself is correctly selected, poor coordination between machines can reduce pellet quality.
A typical EFB pellet production line may include:
EFB Receiving → Cleaning → Shredding → Drying → Crushing → Fine Grinding → Feeding → Pelletizing → Cooling → Screening → Packaging
Every stage should have sufficient capacity.
If the dryer cannot supply enough properly conditioned material, the pellet mill cannot operate consistently.
If the cooler is too small, hot pellets may accumulate after pelletizing.
If the screen is undersized, excessive fines may remain in the finished product.
A balanced production line is therefore essential for maintaining stable pellet quality.
24. Equipment Maintenance
Maintenance has a direct relationship with pellet quality.
Regular inspection should cover:
- Pellet mill
- Die
- Rollers
- Bearings
- Gearbox
- Feeders
- Conveyors
- Dryer
- Grinder
- Cooler
- Screening equipment
A small mechanical problem can eventually become a production-quality problem.
For example, a worn roller may gradually increase the percentage of fines before operators realize that equipment wear is the cause.
Preventive maintenance helps avoid these issues.
Common EFB Pellet Quality Problems
Weak Pellets
Weak pellets can be caused by excessive moisture, insufficient compression, unsuitable particle size, or worn die and rollers.
The production team should check moisture, grinding, die condition, and operating parameters.
Excessive Fines
High fines may result from poor pellet formation, unsuitable moisture, excessive mechanical handling, inadequate cooling, or worn components.
The problem should be diagnosed across the complete production process.
Uneven Pellet Density
Uneven density is often related to inconsistent feeding or variable raw material characteristics.
Improving material preparation and feeding stability can help.
Cracked Pellets
Cracking can occur when pellets are not properly formed or cooled.
Moisture, compression, particle size, and cooling should all be evaluated.
High Ash Content
High ash content may be caused by soil, sand, stones, or other inorganic contaminants mixed with EFB.
Improving raw material cleaning can help produce a cleaner biomass fuel.
How to Maintain Consistent EFB Pellet Quality
Consistent quality requires regular process monitoring.
Operators can establish routine checks for:
- Incoming EFB moisture
- Dried material moisture
- Particle size
- Fiber length
- Pellet mill load
- Die and roller condition
- Pellet temperature after cooling
- Finished pellet moisture
- Pellet durability
- Percentage of fines
Keeping production records allows operators to identify relationships between operating parameters and pellet quality.
For example, if pellet durability decreases after several months of operation, the production team can compare the change with die and roller wear.
How to Improve EFB Pellet Quality
Improving pellet quality does not necessarily require replacing the entire production line.
Several practical improvements can be considered:
Improve Moisture Control
Use an appropriately sized dryer and monitor moisture consistently.
Improve Size Reduction
Reduce long fibers and achieve a more uniform particle size without excessive grinding.
Optimize the Die
Select the correct die diameter and compression ratio for the required pellet specifications.
Stabilize Feeding
Use suitable feeding equipment to prevent bridging and sudden changes in material flow.
Maintain the Pellet Mill
Inspect and replace worn rollers, dies, bearings, and other components as required.
Improve Cooling
Ensure pellets are properly cooled before screening and packaging.
Upgrade Screening
Use an appropriate screening system to remove fines and broken pellets efficiently.
Improve Storage
Protect finished pellets from moisture and unnecessary mechanical damage.
(navigate to this site: RICHI Pelletizer )
Selecting an EFB Pellet Production System
Before purchasing equipment, producers should define their production requirements.
Important considerations include:
- Available EFB quantity
- Initial moisture
- Required production capacity
- Pellet diameter
- Final fuel application
- Factory layout
- Energy availability
- Automation level
- Storage capacity
For small operations, a relatively simple pelletizing system may be sufficient.
For large palm oil mills, an integrated EFB pellet production line can connect drying, grinding, pelletizing, cooling, screening, conveying, and packaging into one continuous process.
A turnkey solution can also include production-line design, equipment manufacturing, installation, commissioning, operator training, and after-sales support.
Conclusion
EFB pellet quality is determined by the interaction of many factors rather than a single machine or operating parameter. Moisture content, particle size, fiber structure, raw material cleanliness, die compression, roller condition, feeding stability, cooling, screening, and storage can all influence the final product.
The pellet mill remains the core of the production process, but it can only perform effectively when the feedstock has been properly prepared. Choosing the right pellet mill, die, and supporting equipment according to the actual characteristics of EFB is essential for producing consistent pellets.
For palm oil mills and biomass fuel producers, effective EFB pellet production begins with understanding the raw material and continues through every stage of processing. By controlling moisture, preparing the material correctly, maintaining stable compression, and managing cooling and storage properly, producers can improve pellet durability, reduce fines, maintain consistent dimensions, and achieve more stable fuel quality.
Ultimately, a well-designed EFB pellet production line should not focus on pellet quality alone. It should balance product quality, production capacity, energy consumption, equipment durability, and operating cost. This approach allows EFB to be transformed from a palm oil processing residue into a more standardized and commercially useful biomass fuel.